
A new method for treating tool bit surfaces that makes an HSS tool bit perform better than a CVD-coated bit.
Less machine chatter and reduced galling enhance life and create a smoother cut, which is always a good outcome.
Quasi-R® and GoldenBlue® treatments reduce friction, improve machining outcomes, and reduce energy waste.
Users report over a 40% reduction in the coefficient of friction and improved hole circularity during drilling.
Easy multi-color tool-bit reconditioning with the cascade e-ion family of machines.
MHI offers GoldenBlue® and Quasi-R® for tooling, parts, and surfaces that need conditioning. This method provides greater hardness, increased wear resistance, and low friction that extends life for a variety of materials and alloys.
Customer testimonial: “We ran one of the inserts on 17-4 stainless steel on our CNC lathe……..The (MHI treatment) coating. “We ran one of the inserts on 17-4 stainless steel on our CNC lathe……..The coating did seem to make a difference. It’s at least 15 to 20% better than without it. I ran the small insert on 1045 steel. Bored 40 pcs with two passes for each bore. One thing I noticed right off the bat was the coating gave an improved finish over a standard insert finish. I did not have to change the insert and finished all 40 pcs without the tool breaking down; it did seem to make a difference. It’s at least 15-20% better than without it. I ran the small insert on 1045 steel. Bored 40 pcs with two passes for each bore. One thing I noticed right off the bat was the coating gave an improved finish over a standard insert finish. I did not have to change the insert and finished all 40 pcs without the tool breaking down!
What is GoldenBlue®?
The Cascade e-ion Plasma is a versatile machine that may be used to impact the surface texture and roughness of metals (Cascade e-Ion source), ceramics (Cascade e-Ion EIZ), or soft plastics (e-Ion LIP). With the e-Ion Plasma machine, one can rapidly “deburr” or create new surfaces, depending on the ions used and other properly set conditions that vary by alloy surface and temperature. Nanoscale texture and porosity features now known to be essential for surface bioactivity or roughness can be engineered. Sometimes, trial-and-error experimentation may be involved, regardless of whether it is HSS, titanium, steel, cobalt, or PEEK alloy. Contact the manufacturer, MHI. The in situ-growth coating that forms when exposed to the cascade e-Ion beam often has low lubricity and high surface hardness. Saves machining energy. It saves tool resources and offers many more benefits. Improved coatings on high-speed machine tools, cutting knives, blades, and even recoating thin razor blades when appropriately coated. Transform and reuse (recoat) at will, re-sharpening when possible. To prolong tool life, identify signs of wear such as abrasion, fracture, chipping, etc. Both thermal and mechanical stresses cause tool wear, with heat and abrasion being the primary culprits. Reducing heat generation during machining by lowering the friction adds considerably to life. You can do this with messy oils or a GoldenBlue®-treated surface.


GoldenBlue® is the trade name for service and multi-color high-value surfaces created by the Cascade e-ion—ultra-hard and ultra-smooth. It delivers a low coefficient of friction (~0.1; number depends on surface) and sharp edges. It achieves a hardness of about 13 GPa and low friction. A hardness of about 13GPa is equivalent to a Rockwell C of about 75 Rc; however, the Rockwell C scale is not meant for such high hardness or coatings. The Cascade e-Ion machines offer easy nano-nitriding/oxynitride of tungsten, cobalt, stainless, and titanium alloys (almost all transition metal alloys) with just air as the process gas (no toxic gas or vacuum treatment).
An extensive surface area treatment, when required, does not present a problem. For example, if railway tracks were made by GoldenBlue® treatment, size would not be a problem. Consider automobile parts, from engine parts to shafts and gears. When you purchase a machine, you are automatically enrolled in the expanding cascade e-ion group knowledge base. The coatings may help prevent bolts and nuts from seizing during operation, i.e., by creating non-seizing surfaces for automobiles, aircraft, and other high-temperature engine parts like bolts, even for corrosive outboards. Each situation may be different. However, MHI will happily provide a limited number of free parts for your verification while this offer lasts. Please contact MHI for details. It is a new type of heat treatment with vast possibilities. MHI has introductory prices well below lasers, large vacuum and gas furnaces, or vacuum ion nitride.
| COATING OXYNITRIDE | e or Carbo-oxynitride variations |
|---|---|
| Color | GoldenBlue® is a trademark that signifies the multi-color hard in situ coating. |
| Structure | Functionally Graded |
| Microhardness | >3000 Vickers (nano) as an example. |
| Applications | It is one of the best for its high hardness, low coefficient of friction, improved drilling speeds, and other benefits, such as less heat and chatter, depending on the substrate. It is used for stainless steel, hardened die steel, and even ceramics. |
Try GoldenBlue®. The process is simple: Immerse or move the part in or under the special CleanElectricFlame™ produced by the Cascade e-Ion™.
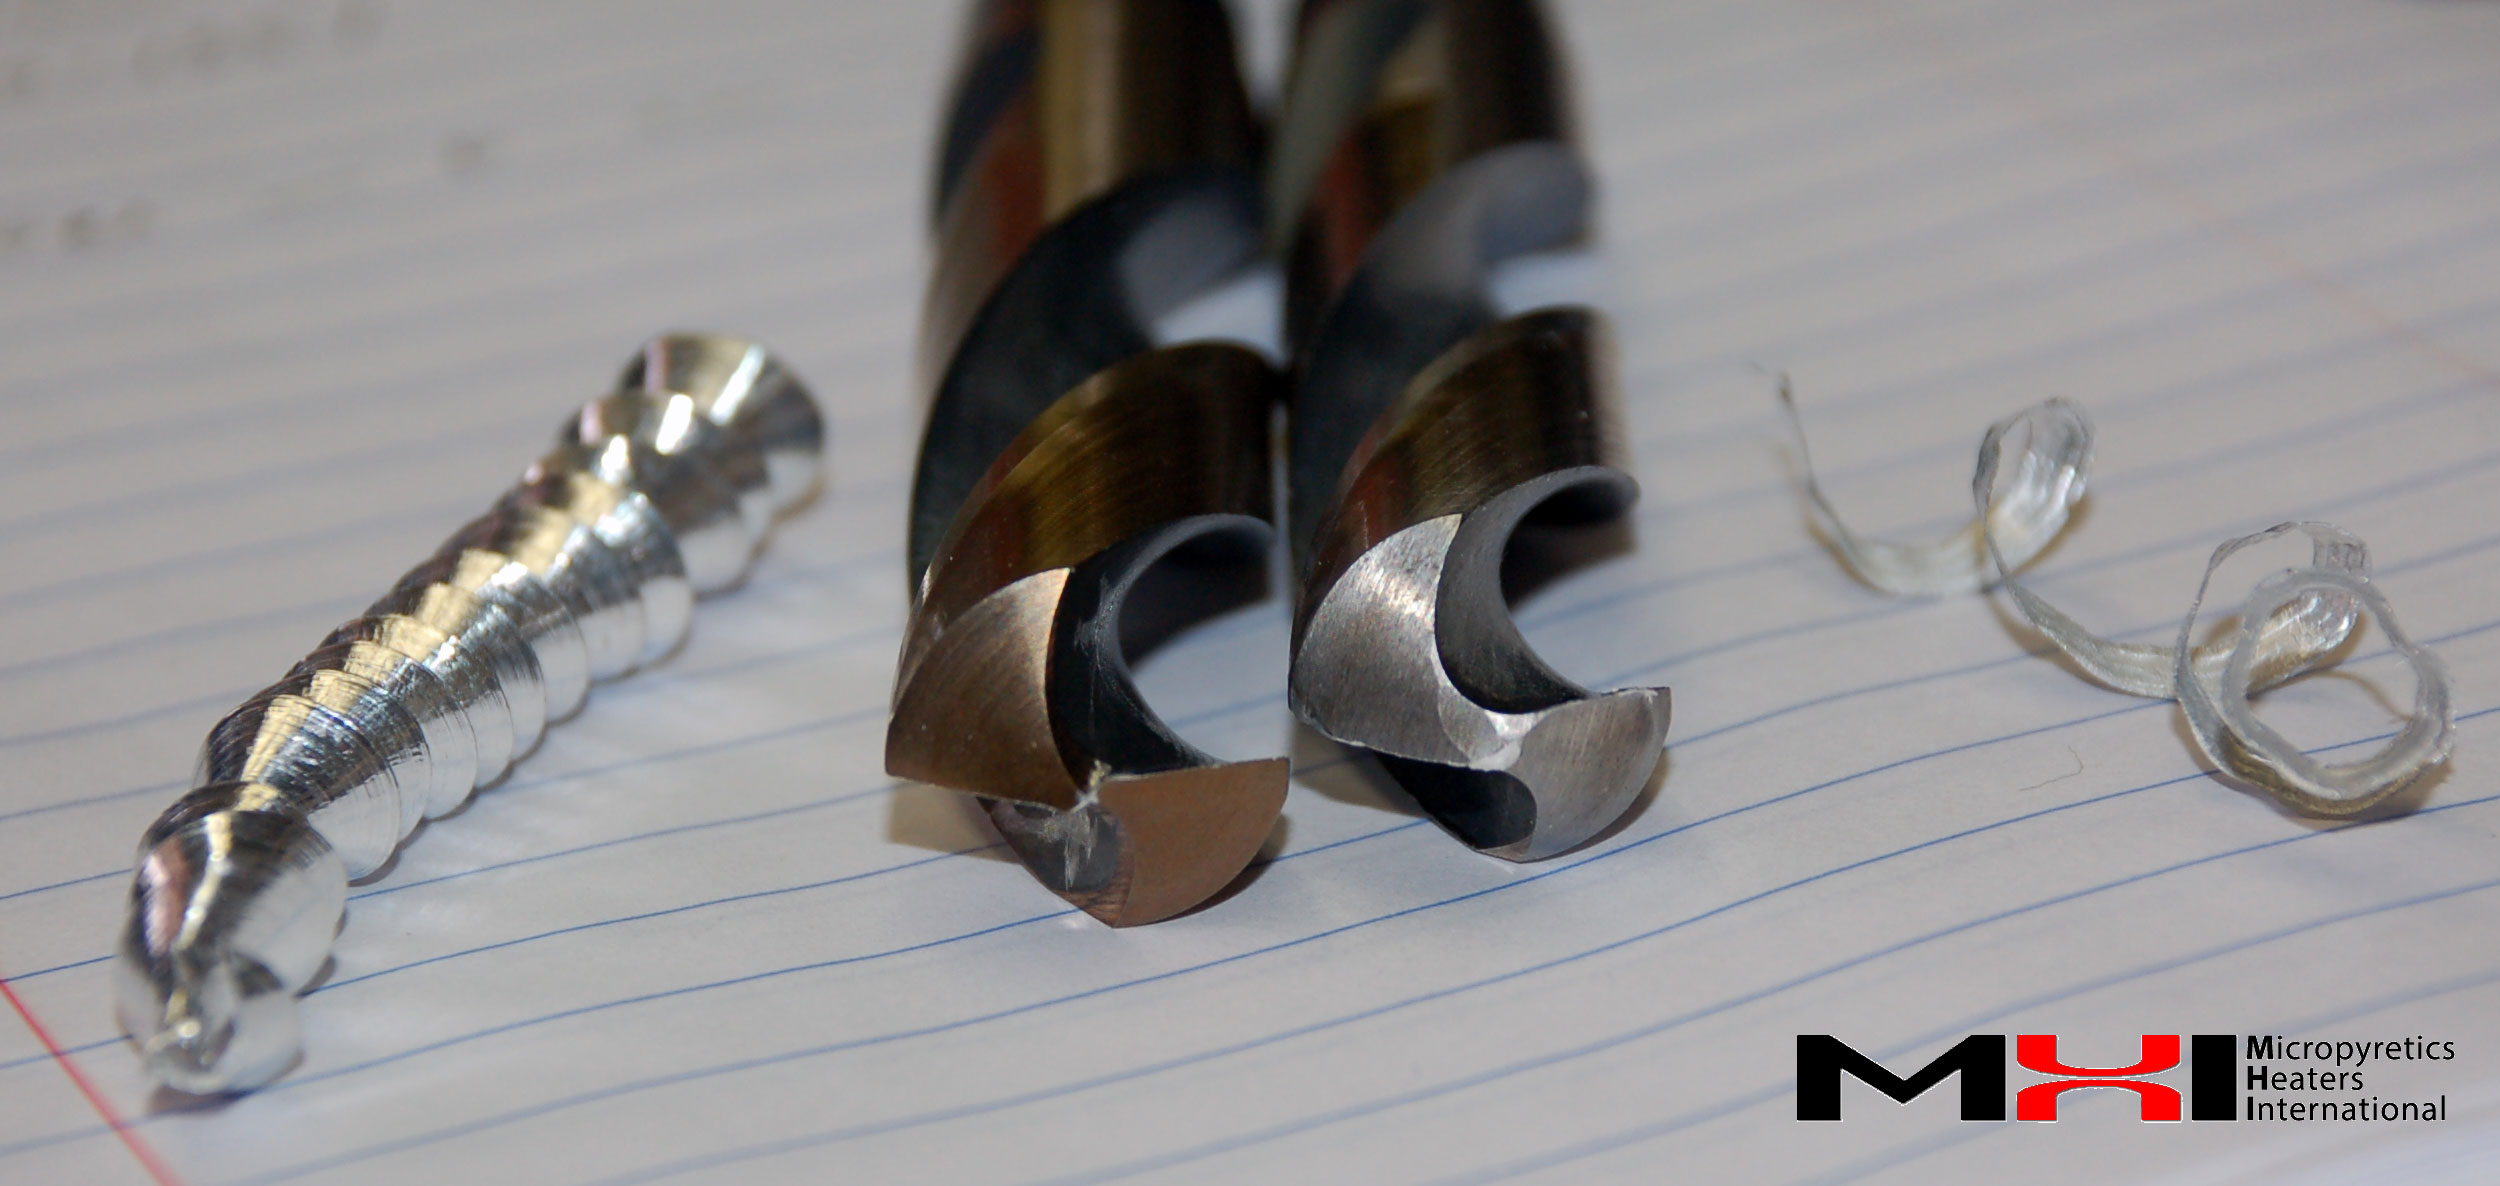


Process for about ten seconds (for a part about an inch thick). For a typical HSS drill bit, expect about a 15% tool life improvement per hole over the uncoated (similar to the range seen with regular TiN or Fe-Ti-Al-N-W-C commercial coatings, at least in our limited trials). The total life improvement could almost double (depending on part size and type). The GoldenBlue® – B treatment offers even better expectations, about a 25% improvement in speed over a regular uncoated HSS. These results are typical and may vary with the drill.
Improve carbide bits: Yes, coating is feasible on end-mill carbide inserts. You can also coat many punches, dies, and other surfaces in situ.
Please send us your specific tool or typical surface for trials so we can treat it for you. We can also determine if your tool bit may be reconditioned to higher grades of GoldenBlue®. A treatment charge is required, which is very nominal.
Early stage, first-time use customer testimonial: “We ran one of the inserts on 17-4 stainless steel on our CNC lathe……..The coating did seem to make a difference. It’s at least 15 to 20% better than without it. I ran the small insert on 1045 steel. Bored 40 pcs with two passes for each bore. One thing I noticed right off the bat was that the coating gave a better finish than a standard insert finish. I did not have to change the insert and finished all 40 pcs without the tool breaking down!
MHI to Customer: Thank you so much for sharing the result.

The available technology for surfaces and tool bits is changing rapidly. How do you compare drills and other tools? The following checklist may assist your evaluation.
(1) For the same sharpness (radius of the edge), compare drill or cutting time; (2) For the same sharpness, compare the life of the tool before it begins to screech or leave behind burns; (3) compare the overall cost of the value addition, i.e., compare the improvement per unit cost including the cost of the of tool, cost of operations, cost of change/wait period, (4) determine whether the tool may be reused after coating and or after re-sharpening, and (5) if applicable, whether a sharpened tool may be recoated.
With Cascade e-Ion-processed tools, we saw better drill speed (we could double the speed in a drilling experiment), improved hole sphericity, cleaner breakthroughs, and smoother tapping control for tapping tools. All this results in more energy efficiency during manufacture and drilling/tapping because of the Goldenblue® treatment/coating.
Is there a simple way to tell whether a Cascade e-Ion Plume-treated part is smoother? Less noise indicates smoothness for a ball bearing, roller bearing, or other part.
How do you know that the surface is harder (or has a higher modulus)? A Vickers hardness test, or bounce a ball bearing and watch if it bounces higher than the untreated one.
With Cascade e-Ion-processed surfaces, we saw improved smoothness, as measured by the chatter quality of the cut, with no seizing and less heat generation. This gives more confidence and longer tool life.
|
Common high-speed steel HSS composition grades (by %wt. nominal) |
||||||||
|
Grade |
C |
Cr |
Mo |
W |
V |
Co |
Mn |
Si |
|
T1 |
0.65-0.80 | 4.00 | – | 18 | 1 | – | 0.1-0.4 | 0.2-0.4 |
|
M2 |
0.95 | 4 | 5 | 6.0 | 2.0 | – | – | – |
|
M7 |
1.00 | 4 | 8.75 | 1.75 | 2.0 | – | – | – |
|
M35 |
0.92 | 4.3 | 5 | 6.4 | 1.8 | 5 | – | 0.35 |
|
M42 |
1.10 | 3.75 | 9.5 | 1.5 | 1.15 | 8.0 | – | – |


Save energy. Repair rapidly at will. Enjoy improved performance.





 MHI Inc. USA
 MHI Inc. USA